

FAQ
-
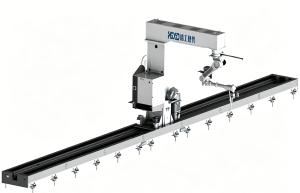
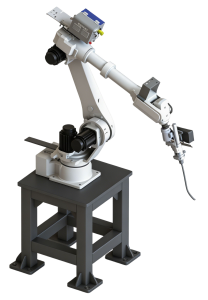
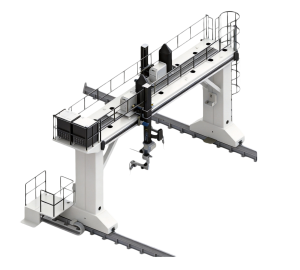
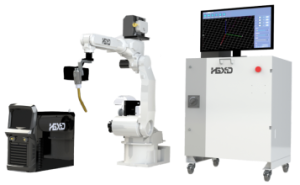
A: Common configurations include fixed, floor-rail, cantilever, gantry, and mobile workstations. The appropriate configuration can be selected based on workpiece dimensions, weld locations, cycle-time requirements, and shop-floor layout.
-
A: Core functions include weld recognition, model import, reverse modeling, high-efficiency precision scanning, template memory, automatic TCP calibration, automatic hand-eye calibration, one-click batch welding, collision detection, digital-twin simulation, data dashboards, mini-program management, and multi-robot coordination.
-
A: They are suitable for small- to medium-sized workpieces where the welds are concentrated within the robot's working range. They feature a compact structure and convenient deployment.
-
A: Key capabilities include multi-industry reverse modeling, high-efficiency precision scanning, template memory and offline templates, physical fixture positioning, curved-groove welding, side-lift side-welding, and digital-twin simulation. Certain functions, including automatic TCP calibration, full-system collision detection, and crater filling, remain under development or are planned for future releases. Please refer to the applicable software version for availability.
-
A: They are suitable for long workpieces or applications requiring welding over a large travel range. With a dual-station layout, loading/unloading and welding can be performed alternately.
-
A: Pricing depends on the selected version, industry package, camera, external axis, welding machine, welding torch, industrial PC, control cabinet, and other configurations. Pricing is not displayed directly on the website. Please contact our sales or pre-sales team for a project quotation.
-
A: Application suitability should be evaluated based on engineering drawings, weld types, plate thickness, accessibility, and on-site conditions.
-
A: Side-mounted cantilever structures are suitable for large, elongated workpieces and can operate across a wider working area. They are commonly used in steel structures, construction machinery, shipbuilding, bridge structures, and transformer oil tanks.
-
A: The system uses a standardized modular design to enable relatively short deployment cycles. Actual delivery time depends on configuration, site conditions, and project complexity. A detailed schedule will be provided by the pre-sales team.
-
A: We recommend providing the workpiece drawings or 3D model, weld locations, plate thickness, production volume, cycle-time requirements, and shop-floor layout. Our pre-sales engineers will then assess the technical limits.
-
A: A multi-axis cantilever adds a lateral travel axis to the standard cantilever, providing wider coverage and making it suitable for large, wide workpieces.
-
A: The system supports data dashboards, mini-program management, and centralized operation and maintenance, allowing one operator to manage multiple machines and reducing labor requirements. The actual number of manageable machines depends on operating conditions and production organization.
-
A: Conditions requiring further evaluation may include workpiece heights exceeding the equipment range, inclined or curved bottom surfaces, plate thickness or weld dimensions outside the standard range, insufficient spacing between stiffeners, obstructed welds, and non-I-type assemblies. Some applications may require manual pre-processing or an alternative solution.
-
A: They are suitable for applications requiring flexible relocation and multi-station operation. They can support both horizontal and vertical welding. Versions supporting side-view and side-welding are better suited to complex operating conditions.
-
A: The system uses high-precision sensors and control systems. Repeatability and weld-bead consistency can meet industrial welding requirements. Specific accuracy specifications are subject to the technical agreement.
-
A: The planar width on both sides of a fillet weld, the angle between stiffeners, and plate thickness can affect vision recognition and welding torch accessibility. Compatibility varies by configuration, so it should be confirmed on a project-by-project basis rather than determined solely from general specifications.
-
A: They should be determined based on the maximum workpiece length, number of workstations, loading/unloading method, and factory layout. Standard floor rails can be customized, with the specific solution assessed by pre-sales engineers.
-
A: The template function saves welding solutions for identical or similar workpieces, allowing them to be recalled directly for subsequent production. This eliminates repeated scanning, modeling, and process verification, making it suitable for batch production and helping improve overall production capacity.
-
A: These are applications that require further evaluation. Feasibility depends on specific dimensions, accessibility, camera field of view, and process configuration. We recommend providing engineering drawings for pre-sales assessment.
-
A: Dual stations allow loading/unloading and welding to alternate, reducing downtime and waiting time while improving equipment utilization and production throughput.
-
A: It supports weaving, intermittent welding, weld resumption, wraparound corner welding, continuous welding, automatic over-weld-hole processing, intelligent arc tracking, multi-layer and multi-pass welding, curved-groove welding, and side-lift side-welding. Functions such as arc restart with retraction, crater filling, and box-girder groove welding are currently under planning.
-
A: Stiffener height and spacing affect the camera's field of view and welding torch accessibility. Different camera mounting configurations have different evaluation criteria. Final selection should be confirmed based on the workpiece drawings and shop-floor layout.
-
A: Attention should be paid to the working range both vertically and parallel to the external axis, as well as positional constraints for flat welding, vertical welding, and openings facing inward or outward. If the working range is exceeded, the workpiece position may need to be adjusted or a larger external axis selected.
-
A: Focusing only on the robot body price while overlooking the overall value of vision, welding processes, software, and external axes; overlooking boundary conditions such as workpiece dimensions, plate thickness, spacing, and weld visibility; overlooking the efficiency benefits of the template function in batch production; and overlooking labor productivity and long-term operation and maintenance costs.
-
A: Common industry solutions include extended wraparound welding, single-side wraparound welding, and circumferential wraparound welding. The appropriate solution depends on plate thickness, end interference, available space, and process requirements.
-
A: Mobile robots can be configured with wheeled, tracked, and tracked floor-rail platforms. The specific platform should be selected based on the workpiece, site conditions, and welding orientation.
-
A: For pricing concerns, emphasize efficiency, labor savings, and flexible welding with reduced teaching requirements. For stability concerns, highlight the fact that the robot body, vision, welding process, and software are provided by the same manufacturer, reducing interface-matching risks. For complex non-standard parts, highlight reverse modeling, automatic weld extraction, and support for multiple welding processes.
-
A: Process capabilities vary depending on the software version, industry package, camera, and external-axis configuration. Specific process capabilities are not individually guaranteed on the website. Please refer to the technical solution and configuration list for the applicable project.
-
A: The system supports assembly-matrix calibration, worktable calibration, hand-eye calibration, and TCP calibration. Automatic TCP calibration is under continuous development, while manual TCP calibration is already supported. Positioner calibration and certain special calibration functions are subject to configuration.
-
A: 3Srobotics holds multiple patents and software copyrights covering robotics, welding, vision, and software, and has received certifications and honors including High-Tech Enterprise and Intelligent Robot Benchmark Enterprise. Specific certificates can be viewed on the Qualifications page of the website.
-
A: Reducing teaching workload is one of the product design objectives. Actual results depend on workpiece characteristics, vision conditions, process configuration, and production volume, and should be evaluated on a project basis.
-
A: The standard configuration typically uses a 2-in-1 camera. A line-scan camera can be selected when higher scanning efficiency is required. Some industry packages require a line-laser camera, with hardware costs charged separately.
-
A: Please provide information such as workpiece drawings or dimensions, weld type, plate thickness, production volume, cycle-time requirements, and shop-floor layout. Our pre-sales engineers will provide a customized selection proposal based on the technical limits and product configuration.
-
A: The template function enables solution reuse for similar workpieces, reducing repetitive preparation. The actual benefits depend on workpiece consistency, production volume, and production setup.
-
A: First, confirm whether workpiece dimensions, plate thickness, weld visibility, and stiffener spacing fall within the technical limits. Then select a fixed, floor-rail, cantilever, multi-axis cantilever, or mobile configuration based on the workpiece length, width, height, and weld locations. Finally, confirm the camera, industry package, process package, and external-axis configuration.
-
A: Under suitable operating conditions, robots can perform continuous welding, helping improve quality consistency and production stability. Actual efficiency and productivity gains vary depending on the workpiece, welding process, and production organization.
-
A: The S Series typically includes the S300 Standard, S600 Advanced, and S900 Flagship versions. The Standard version supports model import; the Advanced version adds multi-industry reverse modeling; and the Flagship version supports multi-robot coordination. Industry packages for applications such as corrugated plates and counterweights are also available.
-
A: Value should be evaluated based on overall efficiency, labor savings, quality consistency, and flexible production capabilities. For a specific project, we recommend having our pre-sales team conduct an ROI assessment.
-
A: Industry packages provide preconfigured processes and functions for specific industry workpieces, such as corrugated plate and counterweight packages. The corresponding upper-level intelligent welding system must be configured before selecting an industry package.
-
A: 3Srobotics provides an integrated system covering the robot body, vision, welding processes, and software, enabling more consistent interface integration, maintenance, and upgrades. Actual stability depends on the specific configuration and on-site conditions.
-
A: The system supports multi-axis standard-mounted robots, cantilever robots, gantry robots, as well as dual-robot coordination, multi-robot coordination, and mobile robot platforms. Specific compatibility is subject to the product configuration table.
Didn’t find your answer?
Tell us about your workpiece, cycle time and site conditions — an application engineer will get back to you with a concrete recommendation.
Contact support